


Page 458 - Ceratizit Catalog
P. 458
MaxiMill 211 system
   B131


             Milling of hard materials (≥ 45 HRC)

             Recommendations for machining                   .  .                              .  .
                                                                (                               (
                                                         l 2                                 l 2
             l
             2


             z


                                                                   a e max
             a e max   = 75%


             Adapter


             Coolant


             Plunging                                     α :  –50%
                                                       R


                                                  f   =  0,05 mm
                                                   z
             Starting values                      v   =  30 - 60 m/min
                                                   c
                                                  a   =  0,5 - 2,5 mm
                                                   p
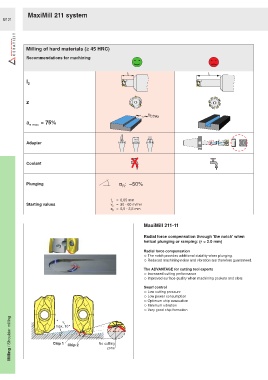
                                                                 MaxiMill 211-11

                                                                 Radial force compensation through 'the notch' when
                                                                 helical plunging or ramping: (r < 2.0 mm)

                                                                 Radial force compensation
                                                                 ○ The notch provides additional stability when plunging.
                                                                 ○ Reduced machining noise and vibration are therefore guaranteed.
                                                                 The ADVANTAGE for cutting tool experts
                                                                 ○ Increased cutting performance
                                                                 ○ Improved surface quality when machining pockets and slots
                                                                 Swarf control
                                                                 ○ Low cutting pressure
                                                                 ○ Low power consumption
                                                                 ○ Optimum chip evacuation
                                                                 ○ Minimum vibration
                                                                 ○ Very good chip formation
      Milling / Shoulder milling  Chip 1  Chip 2  No cutting
                             V
                             f
                          max. 10°


                                                 zone

