


Page 204 - Techniks Catalog 2017
P. 204
Choosing & Using PinzBOHR Boring Heads


            Using 75˚ Boring Heads

            Use a 75-degree head for thru holes when the hole position is accurate.
            A 75-degree head will tend to follow a pre-existing hole. A 75-degree
            head can also be used when there is a lot of stock to be removed.
            The lead angle will allow higher feed rates.

            Using 90˚ Boring Heads

            Use a 90-degree boring head when a hole is off-center, shifted, or off-angle.
            The 90-degree lead angle will have fewer tendencies to follow the existing hole.
            It is also used for blind or stepped holes and is the most versatile of our heads.


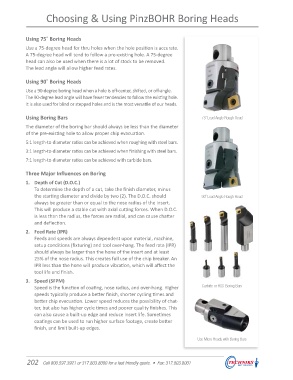
            Using Boring Bars                                                        75˚ Lead Angle Rough Head
            The diameter of the boring bar should always be less than the diameter
            of the pre-existing hole to allow proper chip evacuation.
            5:1 length-to-diameter ratios can be achieved when roughing with steel bars.
            3:1 length-to-diameter ratios can be achieved when finishing with steel bars.

            7:1 length-to-diameter ratios can be achieved with carbide bars.

            Three Major Influences on Boring

            1.  Depth of Cut (D.O.C.)
               To determine the depth of a cut, take the finish diameter, minus
               the starting diameter and divide by two (2). The D.O.C. should        90˚ Lead Angle Rough Head
               always be greater than or equal to the nose radius of the insert.
               This will produce a stable cut with axial cutting forces. When D.O.C.
               is less than the radius, the forces are radial, and can cause chatter
               and deflection.

            2.  Feed Rate (IPR)
               Feeds and speeds are always dependent upon material, machine,
               setup conditions (fixturing) and tool over-hang. The feed rate (IPR)
               should always be larger than the hone of the insert and at least
               25% of the nose radius. This creates full use of the chip breaker. An
               IPR less than the hone will produce vibration, which will affect the
               tool life and finish.
            3.  Speed (SFPM)
               Speed is the function of coating, nose radius, and over-hang. Higher   Carbide or HSS Boring Bars
               speeds typically produce a better finish, shorter cycling times and
               better chip evacuation. Lower speed reduces the possibility of chat-
               ter, but also has higher cycle times and poorer quality finishes. This
               can also cause a built-up edge and reduce insert life. Sometimes
               coatings can be used to run higher surface footage, create better
               finish, and limit built-up edges.


                                                                                    Use Micro Heads with Boring Bars


            202 Call 800.597.3921 or 317.803.8000 for a fast friendly quote.  •  Fax: 317.803.8001

