


Page 423 - Ceratizit Catalog
P. 423
MaxiMill HFC system
                                                                                                                   B96
                                                                                       Application data HFC 12


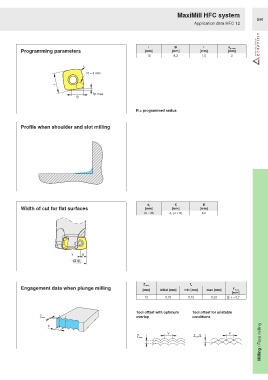
                                                                   l           B           r          a p max
          Programming parameters                                 [mm]        [mm]         [mm]        [mm]
                                                                  12          8,3          1,0          2

                                      r
                                       R = 3 mm

                         l

                                          a p max
                                   B

                                                             R = programmed radius


          Profile when shoulder and slot milling


                                                                               X           B
                                                                   d 1
          Width of cut for flat surfaces                         [mm]        [mm]         [mm]
                                                                 32 - 100   d 1 -(2 x B)   8,3


                                 X    B
                                  Ø d
                                    1


                                                                 Z max               f z
          Engagement data when plunge milling
                                                                [mm]    initial [mm]  min [mm]  max [mm]  Y max
                                                                                                        [mm]
                                                                 10       0,15       0,10      0,20   d 1    x < 0,7

                                                              Tool offset with optimum   Tool offset for unstable
                   Z max                                      overlap                 conditions
                                                                                                                     Milling / Face milling
                      Y
                                                                           Y                           Y
                                                                                        max
                                                              Z max                    Z/2

