


Page 853 - Ceratizit Catalog
P. 853
TC - threading
                                                                                                                   C248
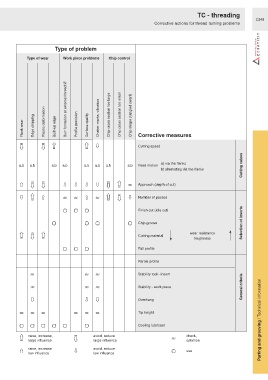
                                                                      Corrective actions for thread turning problems


                         Type of problem

             Type of wear    Work piece problems  Chip control


           Flank wear  Edge chipping  Plastic deformation  Built-up edge  Burr formation at external thread Ø  Profile precision  Surface quality  Chatter marks, vibration  Chip cross section too large  Chip cross section too small  Chip shape (tangled swarf)  Corrective measures


                       ⇪              ⇪       ⇧               Cutting speed
            ⇪
                      ⇪
                                                                                                             Cutting values
                                                                        a) via the flanks
          a,b  a,b      a,b  a,b      a,b  a,b  a,b       a,b  Feed motion
                                                                        b) alternating via the flanks

         ⇧       ⇪    ⇪        ⇧    ⇧    ⇧    ⇧    ⇪  ⇪ ≈     Approach (depth of cut)


              ⇪ ⇧            ≈ ≈ ⇧ ≈ ⇪                  ⇪   ⇧  Number of passes
            ⇧

                             ▢ ▢ ▢                            Finish cut (idle cut)

                        ▢             ▢ ▢                 ▢   Chip groove                                    Selection of inserts

         ⇪       ⇪  ⇪                                         Cutting material       wear resistance
                                                                                       toughness
                             ▢ ▢ ▢                            Full profile


                                                              Partial profile

              ≈                        ≈ ≈                    Stability tool - insert


              ≈                        ≈ ≈                    Stability - work piece                         General criteria


                                                              Overhang
                                              ⇧
                 ⇧
                                         ⇧
          ≈ ≈ ≈                   ≈ ≈ ≈                       Tip height

         ▢ ▢ ▢ ▢ ▢                    ▢                       Cooling lubricant                                      Parting and grooving / Technical information

              raise, increase,             avoid, reduce                            check,
         ⇪ large influence           ⇪     large influence                   ≈      optimise
              raise, increase              avoid, reduce
         ⇧                          ⇧                                        ▢      use
              low influence                low influence

