


Page 830 - Tungaloy Catalog
P. 830
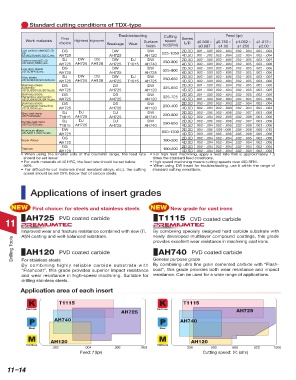
Standard cutting conditions of TDX-type

                                                          Troubleshooting    Cutting                  Feed (ipr)
                                  First                                             Series
                    Work materials      Highfeed Highspeed           Surface   speed      f0.500 -  f0.750 -   f1.062 -   f1.312 -
                                 choice              Breakage  Wear                  L/D
                                                                     finish  Vc(SFM)       f0.687  f1.00   f1.250   f2.00
                  Low carbon steels(C<3)  DS           DW             DW            2D,3D .001 - .005 .002 - .004 .002 - .004  .002 - .004
                  JIS                                                       525-1050
                  SS400,SM490,S25C,etc.  AH725        AH725          AH120          4D,5D .001 - .002 .002 - .004 .002 - .004  .002 - .004
                  Carbon steels(C<3)  DJ  DW    DS     DW      DJ     DW            2D,3D .002 - .005 .002 - .006 .002 - .006  .003 - .007
                  JIS S45C,S55C,etc.  AH725  AH725  AH120  AH725  T1015  AH740  250-800  4D,5D .002 - .003 .002 - .004 .002 - .005  .003 - .006
                  Low alloy steels  DS                 DW             DW            2D,3D .002 - .003 .002 - .005 .002 - .005  .002 - .006
                  JIS SCM415,etc.  AH725              AH725          AH725  525-800  4D,5D .002 - .003 .002 - .005 .002 - .005  .002 - .006
                  Alloy steels     DJ    DW     DS     DW      DJ     DW            2D,3D .002 - .005 .002 - .006 .002 - .006  .003 - .007
                  JIS SCM440,SCr420,etc.  AH725  AH725  AH120  AH725  T1015  AH725  250-650  4D,5D .002 - .003 .002 - .004 .002 - .005  .003 - .006
                  Stainless steels  DS                  DS            DW            2D,3D .001 - .003 .002 - .004 .002 - .005  .002 - .005
                  Austenitic                                                325-650
                  JIS SUS304,SUS316,etc. AH725        AH725          AH120          4D,5D .001 - .003 .002 - .004 .002 - .005  .002 - .005
                  Stainless steels  DS                  DS            DW            2D,3D .001 - .003 .002 - .004 .002 - .005  .002 - .005
                  Martensitic and ferritic                                  325-725
                  JIS SUS430,SUS416,etc. AH725        AH725          AH120          4D,5D .001 - .003 .002 - .004 .002 - .005  .002 - .005
                  Stainless steels  DS                  DS            DW            2D,3D .002 - .003 .002 - .003 .002 - .004  .002 - .004
                  Precipitation hardening                                   250-400
                  JIS SUS630,etc.  AH725              AH725          AH120          4D,5D .002 - .003 .002 - .003 .002 - .004  .002 - .004
                  Gray cast irons  DJ     DJ            DJ            DW            2D,3D .002 - .005 .002 - .006 .002 - .007  .003 - .008
                  JIS FC250,etc.  T1015  AH725        AH725          AH740  250-800  4D,5D .002 - .004 .002 - .005 .002 - .006  .003 - .006
                  Ductile cast irons  DJ  DJ            DJ            DW            2D,3D .002 - .005 .002 - .006 .002 - .007  .003 - .008
                  JIS FCD700,etc.  T1015  AH725       AH725          AH740  250-650  4D,5D .002 - .004 .002 - .005 .002 - .006  .003 - .006
                  Aluminum alloys  DW                                               2D,3D .004 - .006 .006 -.008  .006 - .008  .006 - .010
                  JIS A2017,ADC12,etc.  AH725                               650-1300  4D,5D .003 - .005 .005 - .006 .005 - .006  .005 - .008
                                   DS                                               2D,3D .002 - .004 .002 - .004 .002 - .005  .002 - .006
                  Super Alloys                                              100-200
                                 AH120                                              4D,5D .002 - .004 .002 - .004 .002 - .004  .002 - .005
                                   DS                                               2D,3D .002 - .004 .002 - .004 .002 - .004  .002 - .004
                  Titanium                                                  100-200
                                 AH120                                              4D,5D .002 - .004 .005 - .004 .002 - .003  .002 - .003
                  •  When  using  the  smaller  side  of  the  diameter  range,  the  feed  rate   • For high feed machining, apply a feed rate that is approximately 1.5
                   should be set lower.                                 times the standard feed conditions.
                  • For work materials of 40 HRC, the feed rate should be set below  • High speed machining means cutting speeds over 490 SFM.
                    50%.                                               • When using DW insert for troubleshooting, use it within the range of
                  •  For  difficult-to-cut  materials  (heat  resistant  alloys,  etc.),  the  cutting   standard cutting conditions.
                   speed should be set 25% below that of carbon steels.
                      Applications of insert grades

              NEW     First choice: for steels and stainless steels    NEW New grade for cast irons


           11       AH725  PVD coated carbide                              T1115  CVD coated carbide

                  Improved wear and fracture resistance combined with new (Ti,   By combining specially designed hard carbide substrate with
                  AI)N coating and well-balanced substrate.
                                                                        newly developed multilayer compound coatings, this grade
              Drilling Tools  AH120  PVD coated carbide                 provides excellent wear resistance in machining cast irons.
                                                                           AH740  PVD coated carbide
                  For stainless steels
                                                                        By combining ultra fine grain cemented carbide with “Flash-
                  By combining highly reliable carbide substrate with   General purpose grade
                  “Flashcoat”, this grade provides superior impact resistance   coat”, this grade provides both wear resistance and impact
                  and wear resistance in high-speed machining. Suitable for   resistance. Can be used for a wide range of applications.
                  drilling stainless steels.

                  Application area of each insert

                                 T1115                                               T1115
                    Cast iron                                             Cast iron                        AH725
                                                           AH725
                                AH740                                               AH740

                     Steel                                                 Steel

                              AH120                                                     AH120
                    Stainless                                             Stainless
                               .002         .004        .006       .008               330       500      650      820     1000
                                          Feed: f (ipr)                                      Cutting speed: Vc (sfm)


            11–14            Relating  Cutting Conditions  Technical reference
                             pages
                                         (11-14 )
                                                          (14-1)

