


Page 897 - Tungaloy Catalog
P. 897
11-1 thru 492 - 519:1New Drilling 446-491 8/11/11 5:10 PM Page 519
Drilling Tools
FD - Jet drill for cast irons and aluminum alloy
FDC 519
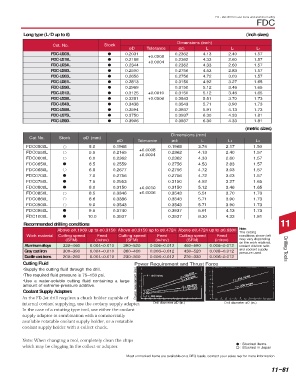
Long type (L ⁄ D up to 8) (inch sizes)
Dimensions (inch)
Cat. No. Stock
øD Tolerance ød1 L L1 L2
FDC-U203L 0.2031 0.2362 4.13 2.40 1.57
FDC-U218L 0.2188 +0.0008 0.2362 4.33 2.60 1.57
+0.0004
FDC-U234L 0.2344 0.2362 4.33 2.60 1.57
FDC-U250L 0.2500 0.2756 4.53 2.83 1.57
FDC-U265L 0.2656 0.2756 4.72 3.03 1.57
FDC-U281L 0.2813 0.3150 4.92 3.27 1.65
FDC-U296L 0.2969 0.3150 5.12 3.46 1.65
FDC-U312L 0.3125 +0.0010 0.3150 5.12 3.46 1.65
FDC-U328L 0.3281 +0.0006 0.3543 5.51 3.70 1.73
FDC-U343L 0.3438 0.3543 5.71 3.90 1.73
FDC-U359L 0.3594 0.3937 5.91 4.13 1.73
FDC-U375L 0.3750 0.3937 6.30 4.33 1.81
FDC-U390L 0.3906 0.3937 6.30 4.33 1.81
(metric sizes)
Dimensions (mm)
Cat No. Stock øD (mm)
øD Tolerance ød1 L L1 L2
FDC0500L 5.0 0.1968 0.1968 3.74 2.17 1.50
+0.0008
FDC0550L 5.5 0.2165 0.2362 4.13 2.40 1.57
+0.0004
FDC0600L 6.0 0.2362 0.2362 4.33 2.60 1.57
FDC0650L 6.5 0.2559 0.2756 4.53 2.83 1.57
FDC0680L 6.8 0.2677 0.2756 4.72 3.03 1.57
FDC0700L 7.0 0.2756 0.2756 4.72 3.03 1.57
FDC0750L 7.5 0.2953 0.3150 4.92 3.27 1.65
FDC0800L 8.0 0.3150 +0.0010 0.3150 5.12 3.46 1.65
FDC0850L 8.5 0.3346 +0.0006 0.3543 5.51 3.70 1.73
FDC0860L 8.6 0.3386 0.3543 5.71 3.90 1.73
FDC0900L 9.0 0.3543 0.3543 5.71 3.90 1.73
FDC0950L 9.5 0.3740 0.3937 5.91 4.13 1.73
FDC1000L 10.0 0.3937 0.3937 6.30 4.33 1.81
Recommended drilling conditions 11
Note:
Above ø0.1969 up to ø0.3150 Above ø0.3150 up to ø0.4724 Above ø0.4724 up to ø0.6300
Drilling
The cutting
Work material Cutting speed Feed Cutting speed Feed Cutting speed Feed conditions shown left
(SFM) (in/rev) (SFM) (in/rev) (SFM) (in/rev) may vary depending
on the work material,
Aluminum alloys 330~460 0.004~0.010 390~520 0.006~0.012 460~590 0.006~0.012 coolant dilution ratio
Gray cast iron 300~390 0.004~0.010 360~460 0.006~0.012 430~520 0.008~0.012 and coolant supply Drilling Tools
pressure used.
Ductile cast irons 200~260 0.004~0.010 230~300 0.006~0.012 230~330 0.006~0.012
Cutting Fluid Power Requirement and Thrust Force
•Supply the cutting fluid through the drill. Work material: Gray cast iron (HB200) Work material: Gray cast iron (HB200)
Cutting speed: V=390 SFM
•The required fluid pressure is 75~150 psi.
•Use a water-soluble cutting fluid containing a large
amount of extreme-pressure additive. Power requirement (kw) Thrust force (N)
Coolant Supply Adapters
As the FD-Jet drill requires a chuck holder capable of
As the FD-Jet drill requires a chuck holder capable of
internal coolant supplying, use the coolany supply adapter. Drill diameter øD (in.) Drill diameter øD (in.)
internal coolant supplying, use the coolant supply
adapter. In the case of rotating-tool type use, use either
In the case of a rotating type tool, use either the coolant
the coolant supply adapter in combination with a
supply adapter in combination with a commercially
commercially available rotatable coolant supply holder,
or a rotatable coolant supply holder with a collect chuck.
available rotatable coolant supply holder, or a rotatable
coolant supply holder with a collect chuck.
Note: When changing a tool, completely clean the chips
which may be clogging in the collect or adapter.
Customer Service: 1-888-554-8394 : Stocked Standard
Note: When changing a tool, completely clean the chips : Non-Stocked Standard
Technical Support: 1-888-554-8391
which may be clogging in the collect or adapter. d : Stocked items.
: Stocked in Japan
Most unmarked items are available on a RFQ basis, contact your sales rep for more information.
11–81

