


Page 813 - Tungaloy Catalog
P. 813
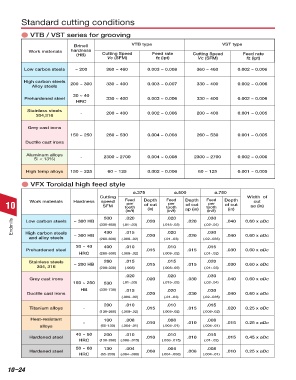
Standard cutting conditions

                  ● VTB / VST series for grooving

                                        Brinell                VTB type                              VST type
                     Work materials   hardness
                                         (HB)       Cutting Speed       Feed rate         Cutting Speed      Feed rate
                                                     Vc (SFM)            fz (ipt)          Vc (SFM)            fz (ipt)

                   Low carbon steels    ~ 200        360 ~ 460        0.003 ~ 0.008       360 ~ 460        0.002 ~ 0.006

                   High carbon steels
                      Alloy steels    200 ~ 300      330 ~ 400        0.003 ~ 0.007       330 ~ 400        0.002 ~ 0.006

                                       30 ~ 40
                   Prehardened steel                 330 ~ 400        0.003 ~ 0.006       330 ~ 400        0.002 ~ 0.006
                                        HRC
                    Stainless steels      -          200 ~ 400        0.002 ~ 0.006       200 ~ 400        0.001 ~ 0.005
                        304,316

                     Grey cast irons
                                      150 ~ 250      260 ~ 530        0.004 ~ 0.008       260 ~ 530        0.001 ~ 0.005
                    Ductile cast irons

                    Aluminum alloys       -         2300 ~ 2700       0.004 ~ 0.008      2300 ~ 2700       0.002 ~ 0.006
                       Si < 13%)

                    High temp alloys  150 ~ 225       60 ~ 125        0.002 ~ 0.006        60 ~ 125        0.001 ~ 0.005

                  ● VFX Toroidal high feed style
                                                                ø.375            ø.500            ø.750
                                                  Cutting    Feed   Depth     Feed    Depth   Feed    Depth    Width  of
                                                                                                                  cut
           10        Work materials    Hardness    speed     tooth   of cut   tooth   of cut  tooth   of cut     ae (in)
                                                                                               per
                                                                               per
                                                             per
                                                    SFM
                                                             (in/t)   (in)    (in/t)  ap (in)  (in/t)  (in)
                                                    500      .020    .020     .020    .020     .030    .040   0.60 x øDc
              Endmills                            (330-660)  (.01-.03)      (.015-.03)       (.02-.04)
                    Low carbon steels
                                        ~ 300 HB
                                                                                               .030
                                                    430
                                                             .015
                                                                              .020
                    High carbon steels
                     and alloy steels   ~ 300 HB  (260-600)  (.008-.02)  .020  (.01-.03)  .020  (.02-.035)  .040  0.60 x øDc
                                        30 ~ 40     400      .010             .010             .015
                    Prehardened steel                                .015             .015             .030   0.60 x øDc
                                          HRC     (280-530)  (.008-.02)     (.008-.02)       (.01-.02)
                     Stainless steels   ~ 200 HB    260      .015    .015     .015    .015     .020    .030   0.60 x øDc
                        304, 316                  (200-330)  (.008)         (.008-.02)       (.01-.03)
                                                             .020             .020             .030
                     Grey cast irons                                 .020             .030             .040   0.60 x øDc
                                       150 ~ 250    530     (.01-.03)       (.015-.03)       (.02-.04)
                                          HB      (330-730)  .015             .020             .030
                    Ductile cast irons                               .020             .030             .040   0.60 x øDc
                                                           (.008-.02)        (.01-.03)       (.02-.035)
                                                    200      .010             .010             .015
                     Titanium alloys       -                         .015             .015             .020   0.25 x øDc
                                                  (130-260)  (.008-.02)     (.008-.02)       (.008-.02)
                      Heat-resistant                100      .008             .008             .008
                                           -                         .010             .010             .015   0.25 x øDc
                         alloys                    (65-130)  (.004-.01)     (.004-.01)       (.004-.01)
                                        40 ~ 50     200      .010             .010             .015
                     Hardened steel                                  .010             .010             .015   0.45 x øDc
                                          HRC     (130-260)  (.008-.015)    (.008-.015)      (.01-.02)
                                        50 ~ 60     130      .004             .004             .008
                     Hardened steel                                  .008             .008             .010   0.25 x øDc
                                          HRC      (65-200)  (.004-.008)    (.004-.008)      (.004-.01)


            10–24         Relating  Cutting Conditions  Technical reference
                          pages
                                                        (14-1)
                                       (10-23)

