Page 852 - Tungaloy Catalog
P. 852

Machining with offset on the lathe


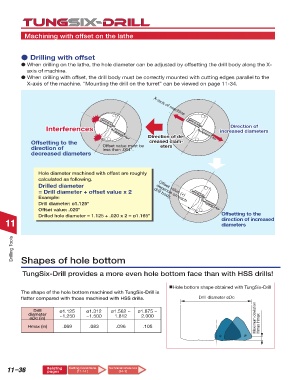
                  ● Drilling with offset
                   When drilling on the lathe, the hole diameter can be adjusted by offsetting the drill body along the X-
                    axis of machine.
                   When drilling with offset, the drill body must be correctly mounted with cutting edges parallel to the
                    X-axis of the machine. “Mounting the drill on the turret” can be viewed on page 11-34.


                                                                        X-axis of machine

                                                                                                        Direction of
                            Interferences         Central edge                        Central edge  increased diameters
                                                                      Direction of de-     Peripheral edge
                                                       Peripheral edge
                      Offsetting to the                                creased diam-
                      direction of                  Offset value must be   eters
                                                    less than .004".
                      decreased diameters


                         Hole diameter machined with offset are roughly
                         calculated as following.
                         Drilled diameter                                  Offset value (+)
                         = Drill diameter + offset value x 2             drill body.    Central edge
                         Example:
                                                                          depends on each
                         Drill diameter: ø1.125"                                            Peripheral edge
                         Offset value: .020"
                         Drilled hole diameter = 1.125 + .020 x 2 = ø1.165"                          Offsetting to the
           11                                                                                        direction of increased
                                                                                                     diameters

              Drilling Tools  Shapes of hole bottom


                  TungSix-Drill provides a more even hole bottom face than with HSS drills!


                                                                                 Hole bottom shape obtained with TungSix-Drill
                  The shape of the hole bottom machined with TungSix-Drill is
                  flatter compared with those machined with HSS drills.                    Drill diameter øDc
                                                                                                                   Maximum deviation
                       Drill      ø1.125     ø1.312    ø1.562 ~   ø1.875 ~
                     diameter
                                                                   2.000
                                  ~1.250
                                             ~1.500
                                                        1.812
                     øDc (in)
                     Hmax (in)     .069       .083       .096       .105                                            Hmax Hmax


            11–36            Relating  Cutting Conditions  Technical reference
                             pages
                                         (11-14 )
                                                          (14-1)
   847   848   849   850   851   852   853   854   855   856   857