


Page 295 - Ceratizit Catalog
P. 295
Types of wear
                                                                                                                   A274


                                                             Flank wear


                                                             Reasons
                                                             ○ Cutting speed too high
                                                             ○  Carbide grade with insufficient wear resistance
                                                             ○ Incorrect feed rate
                                                             Remedies
                                                             ○  Reduce cutting speed
                                                             ○  Select more wear resistant carbide grade
                                                             ○ Adapt feed rate to cutting speed and cutting depth
                                                               (increase feed rate)


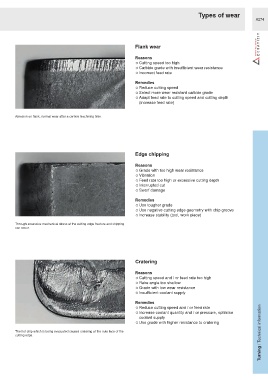
        Abrasion on flank, normal wear after a certain machining time.


                                                             Edge chipping

                                                             Reasons
                                                             ○ Grade with too high wear resistance
                                                             ○ Vibration
                                                             ○  Feed rate too high or excessive cutting depth
                                                             ○ Interrupted cut
                                                             ○ Swarf damage

                                                             Remedies
                                                             ○ Use tougher grade
                                                             ○  Use negative cutting edge geometry with chip groove
                                                             ○ Increase stability (tool, work piece)

        Through excessive mechanical stress at the cutting edge fracture and chipping
        can occur.


                                                             Cratering

                                                             Reasons
                                                             ○  Cutting speed and / or feed rate too high
                                                             ○ Rake angle too shallow
                                                             ○ Grade with low wear resistance
                                                             ○  Insufficient coolant supply
                                                             Remedies
                                                                                                                     Turning / Technical information
                                                             ○  Reduce cutting speed and / or feed rate
                                                             ○ Increase coolant quantity and / or pressure, optimise
                                                               coolant supply
                                                             ○  Use grade with higher resistance to cratering

        The hot chip which is being evacuated causes cratering at the rake face of the
        cutting edge.

