


Page 837 - Tungaloy Catalog
P. 837
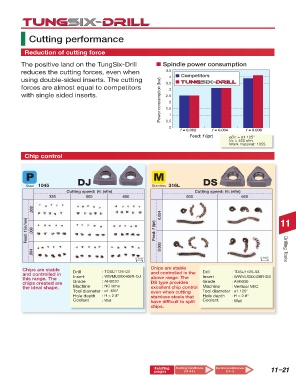
Cutting performance


                   Reduction of cutting force

                  The positive land on the TungSix-Drill                    Spindle power consumption
                  reduces the cutting forces, even when                       4.5   Competitors
                  using double-sided inserts. The cutting                      4
                                                                           Power consumption (kw)  1.5 2
                  forces are almost equal to competitors                      3.5 3
                  with single sided inserts.                                  2.5


                                                                              0.5
                                                                               0 1
                                                                                    f = 0.002    f = 0.004     f = 0.006
                                                                                       Feed: f (ipr)    øDc = ø1.125"
                                                                                                        Vc = 460 sfm
                                                                                                        Work material: 1055

                   Chip control


                                         DJ                                                  DS
                    Steel 1045                                          Stainless 316L
                                     Cutting speed: Vc (sfm)                              Cutting speed: Vc (sfm)
                             325             500            650                       500                    660

                       .008                                                0.004

                    Feed: f (in/rev)  .006                               Feed: f (ipr)                                       11


                                                                           0.003                                               Drilling Tools
                      .004
                                                                 0.100"                                              0.100"
                  Chips are stable                                     Chips are stable
                  and controlled in    Drill       : TDSU1125-03       and controlled in the   Drill     : TDSU1125-03
                  this range. The      Insert      : WWMU08X408R-DJ    above range. The      Insert      : WWMU08X408R-DS
                  chips created are    Grade       : AH9030            DS type provides      Grade       : AH6030
                  the ideal shape.     Machine     : NC lathe          excellent chip control   Machine  : Vertical M/C
                                       Tool diameter  : ø1.125"        even when cutting     Tool diameter  : ø1.125"
                                       Hole depth  : H = 2.8"          stainless steels that   Hole depth  : H = 2.8"
                                       Coolant     : Wet               have difficult to split   Coolant  : Wet
                                                                       chips.


                                                                         Relating  Cutting Conditions  Technical reference  11–21
                                                                         pages       (11-14 )         (14-1)

