


Page 845 - Tungaloy Catalog
P. 845
Cutting performance
Surface finish
Feed: f (ipr)
Tool Tool : TDXCF290L30
0.004 0.005
Work material : Carbon steel
1055 (245HB)
TDS1125-03 (L/D = 3) TDXCF Chamfering width : C = 0.08"
: Vc = 460 sfm
Cutting speed
Machine
: Vertical M/C, CAT40
Coolant
: Wet
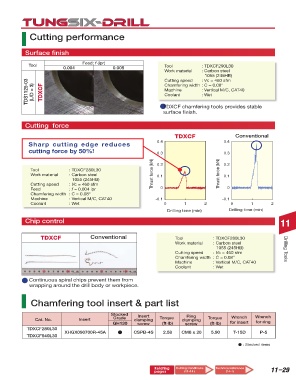
TDXCF chamfering tools provides stable
surface finish.
Cutting force
TDXCF Conventional
0.4 0.4
Sharp cutting edge reduces
cutting force by 50%! 0.3 0.3
Tool : TDXCF280L30 0.2 0.2
Work material : Carbon steel Thrust force (kN) 0.1 Thrust force (kN) 0.1
1055 (245HB)
Cutting speed : Vc = 460 sfm
Feed : f = 0.004 ipr 0 0
Chamfering width : C = 0.08"
Machine : Vertical M/C, CAT40 -0.1 -0.1
Coolant : Wet 0 1 2 0 1 2
Drilling time (min) Drilling time (min)
Chip control 11
TDXCF Conventional Tool : TDXCF280L30
Work material : Carbon steel
1055 (245HB) Drilling Tools
Cutting speed : Vc = 460 sfm
Chamfering width : C = 0.08"
Machine : Vertical M/C, CAT40
Coolant : Wet
Continuous spiral chips prevent them from
wrapping around the drill body or workpiece.
Chamfering tool insert & part list
Stocked Insert Ring Wrench
Cat. No. Insert Grade clamping Torque clamping Torque Wrench
GH130 screw (ft∙lb) screw (ft∙lb) for insert for ring
TDXCF280L30
XHGX090700R-45A CSPB-4S 2.58 CM8 x 20 5.90 T-15D P-5
TDXCF540L30
: Stocked items
Relating Cutting Conditions Technical reference 11–29
pages (11-14 ) (14-1)

