


Page 153 - All Industrial Tool Supply | General Catalog
P. 153
Parobolic Jobbers • DRILLS
                                                                                                               151

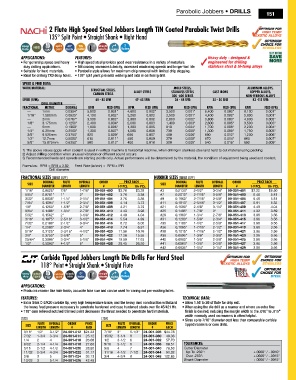
                     2 Flute High Speed Steel Jobbers Length TiN Coated Parabolic Twist Drills
                     135° Split Point • Straight Shank • Right Hand


          APPLICATIONS:         FeATureS:                                              Heavy duty - designed &
          •  For general purpose and heavy   •  High speed steel provides good wear resistance in a variety of materials.  engineered for drilling
           duty drilling applications.  •  TiN coating increases lubricity, increased machining speeds and longer tool life.  stainless steel & hi-temp alloys
          •  Suitable for hard materials.  •  Parabolic style allows for maximum chip removal with limited chip clogging.
          •  Ideal for drilling 7XD deep holes. •  135° split point prevents walking and aids in centering drill.
          SPeeD & FeeD DaTa:
          Work maTeriaL:               STruCTuaL STeeLS,                 moLD STeeLS,                  aLumiNum aLLoyS,
                                        CarboN STeeLS    aLLoy STeeLS   STaiNLeSS STeeLS   CaST iroNS   CoPPer aLLoyS,
                                                                        300 -400 SerieS                NoN-FerrouS aLLoyS
          SPeeD (SFm):                   60 - 85 SFm     47- 65 SFm      36 - 48 SFm     35 - 50 SFm     83 -115 SFm
                  DriLL DiameTer
          FraCTioNaL   meTriC           DeCimaL   rPm   FeeD (iPr)   rPm   FeeD (iPr)   rPm   FeeD (iPr)   rPm   FeeD (iPr)   rPm   FeeD (iPr)
             —     1mm      0.0394"    5,800    0.001"    4,600    0.002"    3,500    0.001"    6,400    0.002"    8,100    0.001"
             1/16"   1.588mm   0.0625"    4,100    0.002"    3,200    0.002     2,500    0.001"    4,400    0.002"    5,800    0.001"
             —     2mm      0.0787"    3,500    0.002"    2,800    0.002     2,000    0.002"    3,800    0.003"    4,900    0.002"
             1/8"   3.175mm   0.1250"    2,400    0.004"    2,000    0.003     1,400    0.003"    2,600    0.005"    3,500    0.003"
             —     5mm      0.1969"    1,600    0.006"    1,200    0.005     910    0.004"    1,700    0.008"    2,200    0.004"
             1/4"   6.35mm   0.2500"    1,300    0.007"    1,000    0.006     730    0.005"    1,300    0.009"    1,750    0.005"
             3/8"   9.525mm   0.3750"    820    0.009"    650    0.007     480    0.006"    890    0.012"    1,200    0.006"
             1/2"   12.7mm   0.5000"    610    0.011"    490    0.009     370    0.008"    670    0.014"    860    0.007"
             5/8"   15.875mm   0.6250"    500    0.012"    400    0.010     300    0.009"    540    0.016"    690    0.009"
          1) The above values apply when coolant is used in vertical machine & horizontal machine, when drilling in stainless steel and hard to cut material using pecking.
          2) Adjust drilling condition when unusual vibration or different sound occurs.
          3) Recommended feeds and speeds are starting points only. Actual performance will be determined by the material, the condition of equipment being used and coolant.
          Formulas:  RPM = SFM x 3.82   Feed Rate (in/min) =  RPM x IPR
                     Drill diameter
          FraCTioNaL SizeS [SeRieS 517P]                         Number SizeS [SeRieS 517P]
                   DeCimaL  FLuTe  overaLL  orDer  ___PriCe eaCH___       DeCimaL  FLuTe  overaLL  orDer  ___PriCe eaCH___
            Size                                                   Size
                  DiameTer  LeNgTH  LeNgTH  #     1-9 PCS.  10+ PCS.     DiameTer  LeNgTH  LeNgTH  #     1-9 PCS.  10+ PCS.
           1/16"   0.0625"  7/8"  1-7/8"  09-051-400  $3.76  $3.38  #3    0.2130"  2-1/2"  3-3/4"  09-051-401  $7.22  $6.50
           5/64"   0.0781"  1"    2"    09-051-402  3.76  3.38     #7     0.2010"  2-7/16"  3-5/8"  09-051-403  6.46  5.81
           3/32"   0.0938"  1-1/4"  2-1/4"  09-051-404  3.76  3.38  #9    0.1960"  2-7/16"  3-5/8"  09-051-405  6.46  5.81
           7/64"   0.1094"  1-1/2"  2-3/4"  09-051-406  4.14  3.73  #11   0.1910"  2-5/16"  3-1/2"  09-051-407  5.91  5.32
           1/8"    0.1250"  1-5/8"  2-7/8"  09-051-408  4.21  3.79  #21   0.1590"  2-1/8"  3-1/4"  09-051-409  4.49  4.04
           9/64"   0.1406"  1-3/4"  2-7/8"  09-051-410  4.43  3.98  #25   0.1495"  1-7/8"  3"  09-051-411  4.32  3.89
           5/32"   0.1562"  2"    3-1/8"  09-051-412  4.49  4.04   #29    0.1360"  1-3/4"  2-7/8"  09-051-413  3.96  3.56
           3/16"   0.1875"  2-5/16"  3-1/2"  09-051-414  5.54  4.99  #31  0.1200"  1-5/8"  2-3/4"  09-051-415  3.96  3.56
           7/32"   0.2188"  2-1/2"  3-3/4"  09-051-416  6.72  6.05  #35   0.1100"  1-1/2"  2-5/8"  09-051-417  3.96  3.56
           1/4"    0.2500"  2-3/4"  4"  09-051-418  7.74  6.97     #36    0.1065"  1-7/16"  2-1/2"  09-051-419  3.96  3.56
           5/16"   0.3125"  3-3/16"  4-1/2"  09-051-420  11.96  10.76  #38  0.1015"  1-7/16"  2-1/2"  09-051-421  3.96  3.56
           3/8"    0.3750"  3-5/8"  5"  09-051-422  17.28  15.55   #39    0.0995"  1-3/8"  2-3/8"  09-051-423  3.96  3.56
           25/64"  0.3906"  3-3/4"  5-1/8"  09-051-424  19.59  17.63  #40  0.0980"  1-3/8"  2-3/8"  09-051-425  3.96  3.56
           1/2"    0.5000"  4-1/2"  6"  09-051-426  29.45  26.50   #41    0.0960"  1-3/8"  2-3/8"  09-051-427  3.96  3.56
                                                                   #42    0.0935"  1-1/4"  2-1/4"  09-051-429  3.96  3.56
                  Carbide Tipped Jobbers Length Die Drills For Hard Steel
                  118° Point • Straight Shank • Straight Flute


          APPLICATIONS:
          •  Produces reamer like hole finish, accurate hole size and can be used for coring out pre-existing holes.
          FeATureS:                                                         TeChNICAL DATA:
          •  Extra thick C-2/K20 carbide tip, very high temperature braze, and the heavy land construction withstand   •  Allow 1.5Ø to 2Ø of flute for chip exit.
           the heavy feed pressure necessary to penetrate hardened and case hardened steels over Rc 45/421 Hb.  •  When using the die drill as a reamer and where an extra fine
          •  118° cam relieved notched thinned point decreases the thrust needed to penetrate hard materials.  finish is desired, reducing the margin width to the .010" to .015"
                                                                              width normally used on reamers is often helpful.
          [150]                            [150]                            •  Sizes up to 7/16" diameter cost less than comparable carbide
                 FLuTe  overaLL  orDer  PriCe     FLuTe  overaLL  orDer  PriCe
            Size                             Size                             tipped reamers or core drills.
                LeNgTH  LeNgTH  #   eaCH         LeNgTH  LeNgTH  #    eaCH
           3/16"  1/2"  3-1/2"  24-001-012 $24.33  7/16"  3"  5-1/2"  24-001-028 $44.78
           7/32  1-3/4  3-3/4  24-001-014  25.12  15/32  3-1/4  6  24-001-030  49.36
           1/4  2     4    24-001-016  26.08  1/2  3-1/2  6  24-001-032  57.70
           9/32  2-1/4  4-1/4  24-001-018  27.60  9/16  3-1/2  6  24-001-036  68.51  ToLeraNCeS:
           5/16  2-1/2  4-1/2  24-001-020  28.80  5/8  4  7  24-001-040  78.68  Cutter Diameter
           11/32  2-3/4  4-3/4  24-001-022  31.17  11/16  4-1/2  7-1/2  24-001-044  91.02    Up To .250":   +.0000" / -.0010"
           3/8  3     5    24-001-024  33.13  3/4  4-3/4  8  24-001-048 102.85    Over .250":             +.0000" / -.0015"
           13/32  3   5-1/4  24-001-026  42.49                               Shank Diameter               +.0000" / -.0015"

